Business Details
34 Years
experience
Expert Industrial Flooring Solutions in Ontario
Abate & Associates has been serving Ontario since 1992, delivering comprehensive flooring solutions tailored to industrial and commercial needs. Our team combines over 50 years of collective expertise with advanced techniques and equipment to address diverse flooring challenges, from epoxy coatings to polyurethane cement installations. We prioritize safety, value, and customer satisfaction, utilizing dust-free shotblast technology and a full range of products to ensure durable, chemically resistant surfaces. Our approach includes professional consultation, precise surface preparation, and customized finishes, including anti-skid textures and decorative options. With a focus on thermal shock resistance and moisture tolerance, we serve sectors like food and beverage, pharmaceuticals, and heavy industry.Our polished concrete solutions offer eco-friendly, low-maintenance flooring with high-gloss aesthetics. We specialize in addressing substrate contamination risks and chemical exposure through advanced coating systems. Our commitment to quality extends to steam-cleanable installations and temperature-resistant materials. By understanding each client's unique operational demands, we recommend systems optimized for abrasion resistance and longevity. As a trusted partner, we ensure every project meets rigorous industry standards while maintaining transparency and reliability.
Services
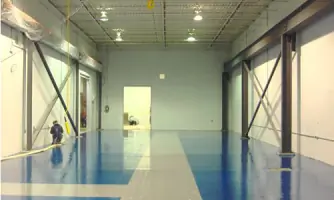
Epoxy Flooring
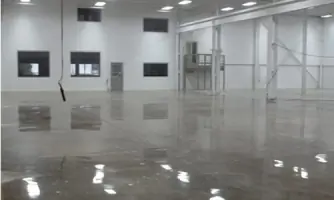
Polished Concrete
Polyurethane Cement
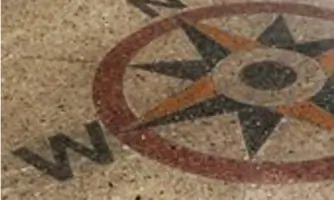
Decorative Quartz
MMA Flooring
Details
- Year established: 1992
Highlights and features
- We have over 50 years combined experience in industrial flooring solutions
- Our team operates a full fleet of dust-free shotblast equipment
- We offer comprehensive product selection for customized flooring needs
- Our professionals handle projects from consultation to installation
- We specialize in thermal shock-resistant flooring systems for extreme environments
Services
Epoxy Flooring
Epoxy flooring systems provide durable, chemical-resistant surfaces for industrial environments. Our installations enhance abrasion resistance while maintaining easy-clean properties. Customizable with anti-skid textures and color-matching options, these fast-curing coatings minimize facility downtime. Ideal for food processing plants and chemical handling areas, our epoxy solutions protect concrete substrates from oil penetration and premature deterioration.
Polished Concrete
Our diamond polishing process transforms concrete into low-maintenance, high-gloss flooring. Using metal and resin-bonded diamonds, we achieve customizable aggregate exposure and shine levels. The eco-friendly system includes concrete densification and protective sealing. Suitable for new installations or refurbishing existing floors, this solution offers thermal shock resistance and compatibility with water-based staining for decorative effects.
Polyurethane Cement
Specialized polyurethane cement flooring withstands extreme temperatures (-40C to 120C) and chemical exposure. Ideal for freezers, dairies, and chemical plants, our installations resist organic acids, solvents, and thermal shock. The system accommodates moisture vapor transmission while maintaining structural integrity. Steam-cleanable at - inch thickness, these floors combine durability with hygiene compliance for food processing environments.
Questions
What industries do you specialize in?
We serve food and beverage facilities, pharmaceutical plants, automotive manufacturers, chemical processing units, and heavy industrial operations across Ontario.
How do your epoxy coatings improve safety?
Our systems incorporate anti-skid textures for wet areas and chemical-resistant barriers that prevent substrate contamination while maintaining slip resistance.
Can you refurbish existing concrete floors?
Yes, our diamond polishing process revitalizes old concrete through multi-stage grinding, densification, and protective sealing without replacement.
What temperature ranges do your floors handle?
Polyurethane cement systems operate effectively between -40°C and 120°C, with epoxy solutions maintaining stability under standard industrial conditions.